
 ES
Marble is soft enough to grind quickly and sensitive enough to punish impatience. Press a hard metal-bond wheel into it and the stone scorches; let an open segmented wheel catch an edge and it chips. A coarse resin filled cup wheel avoids both problems, because its continuous face glides over the stone instead of biting it, cutting cool and leaving a surface ready for finer grits.
What 'coarse resin filled' means for marble
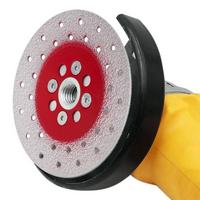
The wheel has a continuous working face, with the gaps between segments filled with resin, so there is no open edge for the stone to catch on. The resin also runs cooler than a metal bond, which matters on marble because heat discolours and burns the surface. The 'coarse' refers to the diamond grit - large grains that remove material quickly and leave a fairly deep scratch pattern. A coarse resin filled cup wheel for granite and marble is built for exactly this first stage.
Why marble wants a resin face
- Cooler cutting: marble burns and discolours under friction, so a cool-running bond protects the surface.
- No snagging: the filled face has no open gullets, so edges and veined areas are far less likely to chip.
- Even scratch pattern: continuous contact leaves a consistent finish rather than the deep gouges an open segment can make.
- Forgiving feed: resin filled wheels tolerate a steadier hand than a very aggressive metal wheel, which suits the careful work marble needs.
Where coarse grinding fits the sequence
Coarse grinding is the first stage of restoring or levelling a marble surface. It removes the deep scratches, lippage between tiles, surface staining and the remnants of an old finish. From there the work steps down through progressively finer grits - finer cup wheels or resin pads - until the stone reaches the required gloss. Skipping the coarse stage leaves deep scratches that finer grits cannot remove; staying on the coarse stage too long leaves scratches the finer grits must then work harder to erase. Getting the sequence right is what makes the finish predictable. See resin filled vs metal bond cup wheels for how the stages fit together.
Using a coarse resin filled wheel on marble
- Keep the wheel flat on the surface and move in overlapping passes; tilting the wheel digs a hollow.
- Let the diamond cut - do not press hard, which heats the stone and loads the machine.
- Keep water or a suitable coolant flowing to control heat and flush the slurry, especially on marble.
- Work the whole surface evenly rather than chasing one scratch, or you create a dip.
- Check progress often; stop as soon as the required depth is reached and move to the next grit.
Safety
Marble dust is a respiratory hazard and grinding creates both dust and slurry, so wear a dust mask or respirator, eye protection and hearing protection, and control the dust with water or extraction. Use the grinder guard and side handle, respect the wheel's maximum RPM, clamp the workpiece and follow the manufacturer's instructions. On a wet polisher, keep water away from electrical connections and use an RCD or GFCI.
Coarse marble grinding in short
- Coarse resin filled wheel for the first, material-removing stage.
- Cool, controlled cut that avoids chipping and burning.
- Follow with progressively finer grits to the required finish.
- Keep the wheel moving, keep it cool, and control the dust - browse the grinding disc range for the stages that follow.