
 ES
Two blades can sit side by side on a shelf at very different unit prices and still be the wrong and the right purchase — in either order. Unit price tells you what leaves the account today. Cost per cut tells you what the tool costs to actually use, and that is the number that shows up in a shop's overheads.
This is a method for working that number out, and for knowing when the number is not worth calculating at all.
What cost per cut actually is
The calculation is simple; the discipline is in the inputs.
cost per unit of work = (tool cost + changeover cost) ÷ work completed
"Work completed" is whatever unit matches the job: cuts, linear metres, square metres, or holes. Tool cost is the purchase price of one tool. Changeover cost is the labour and downtime involved in swapping it out — a figure most buyers leave out, and the one that most often reverses the answer.
The result is only comparable if both tools were measured on the same material, the same machine and the same job. Comparing a figure from a clean bench test against a figure from a site with interrupted cuts tells you nothing useful.
Pick the unit before you start counting
Choose the unit first, then count against it consistently. For a masonry blade used on kerb cuts, cuts are the natural unit. For floor grinding, square metres. For core drilling, holes or drilled depth. For stone fabrication, linear metres of edge.
Mixing units mid-comparison is the most common way a cost-per-cut exercise quietly becomes meaningless.
Collecting numbers that hold up
Measure on a real job rather than a demo. Note the material, the machine, the operator and the water supply, because each of them changes the result. Count the work completed until the tool is genuinely finished — not until it feels slower, but until it stops cutting at an acceptable rate or reaches its wear limit, whichever comes first.
Record the reason the tool was retired. A blade that glazed out because of too little water was not worn out; it was used outside its range, and that is a process finding rather than a product finding.
What actually moves the denominator
Several variables sit between the specification sheet and the result, and they matter more than most buyers expect:
- Material hardness and abrasiveness — the same blade on cured concrete and on soft brick are not comparable runs
- Machine power and RPM, and whether the blade is run at a speed it is rated for
- Water supply and cooling, which decide whether the bond keeps shedding
- Operator technique, especially feed rate and whether the tool is forced
- Glazing, which shortens the effective life without the tool being worn
- Segment height, since a taller segment simply contains more usable diamond
Of these, segment height is the easiest to compare on paper, and it is the one buyers most often overlook.
Segment height as a value signal
Two blades of the same diameter and rim type can carry noticeably different segment heights. Since segment height is roughly the useful life of the tool, dividing the blade price by the segment height gives a rough cost per millimetre of usable diamond — a more honest comparison than price per blade.
It is a rough figure, not a life prediction, because wear rate still depends on the material and how the blade is run. But when two quotes look similar and one has a much shorter segment, the comparison has already told you something.
The costs beyond the tool
Cost per cut only counts the tool. The costs that surround it often dominate:
- Downtime while a tool is changed, including the time to find a replacement
- Rework caused by a finish the customer rejects
- Wasted material, where a bad cut damages stock worth more than the tool
- Returns and the handling that goes with them
- Labour, which usually costs far more per hour than the blade consumes per cut
That last point is worth stating plainly: if a slower blade adds even a small amount of labour per cut, the labour cost will often exceed the difference in tool price well before the blade is worn out.
When cost per cut is the wrong metric
For cutting and grinding, cost per unit of work is a reasonable way to compare. For polishing and finishing it usually is not, because the variable that matters is rework rate rather than consumption. A pad that lasts longer but leaves haze costs more in labour than it saves in pad price. Judge finishing tools on how often the edge has to be redone.
A worksheet you can run
Take three candidate tools. For each one, on the same job: record the purchase price, note the segment height or the relevant wear dimension, count the work completed before retirement, and add an estimate of changeover time valued at the shop's labour rate. Divide. Compare the three figures, and compare the reasons each tool was retired.
Then sanity-check the result against the labour involved. If the numbers say a slow tool is cheaper but the crew finished later, trust the crew.
What a comparison like this cannot do is promise a specific service life. Actual performance depends on the machine, the material, the feed rate, cooling and operator technique, so treat any published life figure with suspicion unless the conditions are stated alongside it.
What to ask a supplier
A cost-per-cut comparison is only possible if the supplier gives you the inputs: segment height, bond type, rim design and rated speed, for each size in the range. For importers building a range, ask the same questions across the whole line so the comparison holds between sizes, and confirm which sizes share a common bond. Purchase terms, sample arrangements and delivery timing should be confirmed directly with the supplier rather than carried over from another vendor.
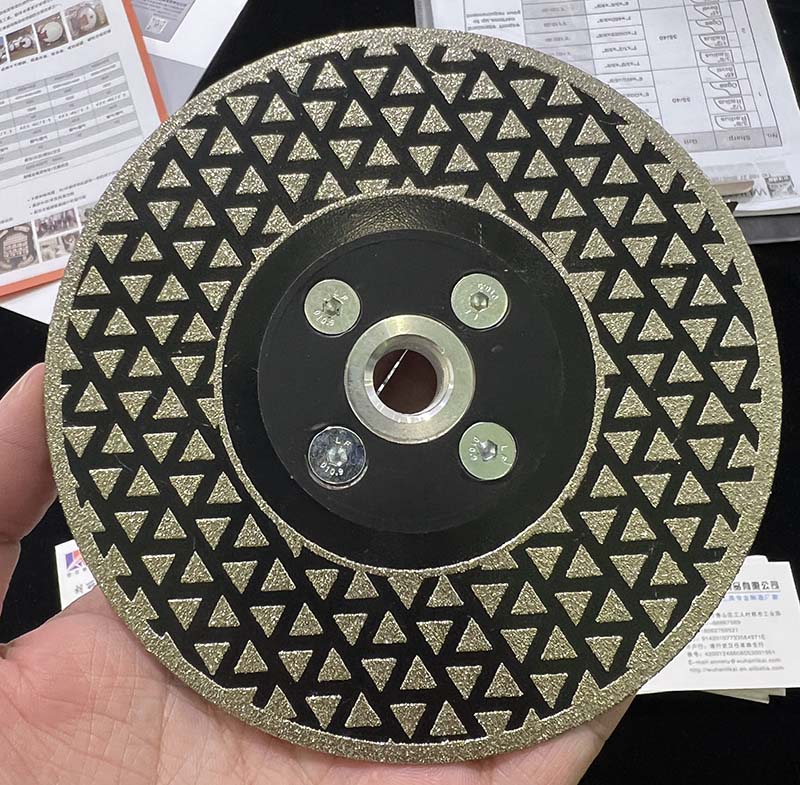
Start from the diamond saw blade range or the cutting disc range, and read the specifications by size rather than by price. A turbo cutting and grinding disc and a double sided cutting disc are useful reference points for what a specification sheet actually contains; on the finishing side, polishing pads for granite and stone belong in a rework-based comparison rather than a cost-per-cut one.
Three related guides extend this: segment height and blade value, how to read blade labels and technical markings, and the wider wholesale checklist for importers and distributors.
If you want a specification sheet that supports a like-for-like comparison across a range, ask for the segment height, bond and rated speed per size before quoting.